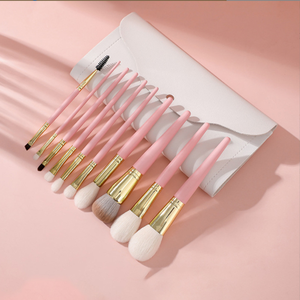
Seamless Anodized Rose & Pink Aluminum Ferrules
- Material: High-Grade AL 6063-T5
- Finish: Anodized Color Match
- Wall Thickness: 0.35mm - 0.50mm
Explore our foundational range of custom aluminum ferrules, metal sleeves, and high-performance brush connectors crafted with tolerances down to ±0.02mm.
In modern cosmetic manufacturing, specialized industrial brushcraft, and technical applicator assembly, the aluminum ferrule serves as the structural nexus binding functional bristles to ergonomic handles. Precision engineering in ferrule geometry, grain boundary alignment, crimp tensile retention, and electrochemical anodizing directly dictates product longevity, brand aesthetic value, and end-user performance consistency.
Custom aluminum ferrule production requires an intimate technical balancing act between metal ductility, structural tensile strength, corrosion immunity, and surface finishing receptivity. Unlike generic copper or cheap rolled steel, high-purity aluminum alloys offer optimal strength-to-weight ratios and superior electrochemical oxidation properties.
Depending on your application—whether ultra-lightweight cosmetic brush kits, high-pressure industrial cleaning brushes, or chemical-resistant art tools—selecting the proper aluminum substrate is paramount. Below is our engineering evaluation matrix:
| Aluminum Grade | Yield Strength (MPa) | Ductility / Formability | Anodizing Performance | Primary Industrial Application |
|---|---|---|---|---|
| AL 1050 / 1060 | 35 - 85 | Exceptional (High Draw) | Bright Mirror Finish | Deep-drawn seamless cosmetic ferrules |
| AL 3003 | 90 - 145 | Excellent | Good Matte / Colored | Standard beauty tools & promotional sets |
| AL 6063-T5 | 145 - 200 | Moderate (Machinable) | Superior Hard Anodizing | Heavy-duty groomers, premium handles |
| AL 6061-T6 | 240 - 290 | Limited Forming | Technical Coat Ready | High-stress industrial & aerospace applicators |
For seamless ferrules, AL 1050 and 1060 remain the industry standard for deep-drawing processes. Their high purity allows metal blank discs to be drawn through progressive carbide dies without stress cracking, producing wall thicknesses down to 0.25mm while maintaining structural integrity during mechanical crimping.
Our 20,000 m² factory employs automated multi-station deep-drawing equipment alongside high-speed precision tube-cutting machines. Understanding how your aluminum ferrules are manufactured ensures optimal budget allocation and technical fit.
Fabricated from a single flat circular aluminum disc using sequential hydro-hydraulic punch presses. Eliminates all side seams, guaranteeing 100% leak-proof liquid isolation and uniform 360-degree radial crimping strength.
Formed from extruded precision aluminum tubing cut to micro-length tolerances via CNC flying saws. Ideal for straight cylindrical collars, double-ended brush sleeves, and cost-effective high-volume contract orders.
Secondary automated pressing shapes round ferrule ends into flat, oval, angled, or pinched profiles. Enables unique bristle flare geometry while preserving internal cavity retention forces.
The visual appeal and chemical resistance of an aluminum ferrule depend on surface treatment. Raw aluminum rapidly forms a natural thin oxide film, but industrial applications demand engineered electrolytic passivation.
As global brand supply chains face heightened scrutiny over environmental impact, traceability, and lead-time risks, B2B purchasing directors are shifting procurement strategies toward certified OEM partners who offer real technical innovation.
Global beauty conglomerates are mandating 30% to 100% PCR aluminum usage. Utilizing recycled aluminum cuts energy consumption during metal smelting by up to 95%, drastically lowering Scope 3 carbon footprints without compromising tensile ductility.
Traditional glue-only assembly is being superseded by dual-zone internal micro-grooving. Precision internal circumferential ribs lock into wooden or synthetic handles, raising pull-off force resistance by over 40% while reducing chemical adhesive dependence.
Tier-1 factories are abandoning manual batch sampling in favor of 100% high-speed optical camera sorting. Automated systems inspect ovality, wall thickness, rim burrs, and color hue uniformity at speeds of 600 pieces per minute.
Backed by over 30 years of specialized manufacturing experience, our state-of-the-art facility operates under Korean precision engineering standards. We bridge high-capacity volume output with bespoke artisan customization.
| Certification standard | Audit focus & Operational scope | Direct Buyer Benefit |
|---|---|---|
| ISO 9001 | Quality Management Systems & Process Consistency | Guaranteed lot-to-lot dimensional uniformity and zero defect targets. |
| ISO 14001 | Environmental Management & Waste Reduction | Eco-compliant chemical anodizing wastewater treatment. |
| ISO 45001 | Occupational Health & Workplace Safety | Stable, risk-free manufacturing continuity for enterprise buyers. |
| SA8000 | Social Accountability & Ethical Labor Practice | Seamless compliance with international ESG retailer audits. |
| FSC CoC | Chain of Custody for Wood & Packaging Compatibility | Full integration with certified sustainable wooden handles. |
| EcoVadis Rating | Corporate Social Responsibility & Sustainable Procurement | Verified Tier-1 sustainability credentials for global brands. |
Get clear, definitive technical answers regarding OEM custom tooling, order minimums, surface longevity, and international logistics.
For standard stocked diameters (e.g., 6mm, 8mm, 10mm, 12mm, 18mm, 24mm) with standard anodized silver or gold finishes, our baseline MOQ starts at 5,000 to 10,000 units. For completely custom drawn sizes requiring dedicated progressive die tooling or specialized custom pantone anodizing, the MOQ is generally 30,000 units per specification. We offer flexible pilot run prototyping for qualified OEM development programs.
Our factory utilizes high-precision carbide drawing dies and automated CNC trimming lathes. Dimensional tolerances are held within ±0.02mm for inner diameter (ID) and outer diameter (OD), and ±0.05mm for overall length. Continuous optical vision sensors measure concentricity during production to guarantee seamless fit over handles and easy insertion of bristle hair knots.
Yes. Properly anodized aluminum ferrules undergo electrolytic sealing in hot deionized water or nickel acetate solutions, closing the microscopic aluminum oxide pores. This renders the surface inert to cosmetic alcohols, brush cleansing detergents, synthetic solvents, and moisture. Our products pass 48-hour ASTM B117 salt spray corrosion testing without pitting or color degradation.
Custom 3D prototyping and CAD drawing sign-offs require 3–5 working days. Rapid sample die creation and initial physical sample delivery take approximately 10 to 14 days. Once pre-production samples are approved, full-scale mass production lead time averages 25 to 35 days, supported by our 800,000-unit monthly production capacity.
Absolutely. We source certified Post-Consumer Recycled (PCR) aluminum billets and coils that conform to international environmental standards. Combined with our FSC-certified wooden handle assembly solutions and EcoVadis-rated facility practices, we provide complete sustainable OEM packaging configurations ready for global retail distribution.
We provide four primary branding methods: (1) High-speed Fiber Laser Engraving for precise permanent metallic logos; (2) Mechanical Die Stamping / Embossing for raised or recessed textures; (3) Rotational Silk-Screen Printing using epoxy-based metallic inks; and (4) Anodized Masking to create dual-tone polished/matte contrast logos.
Partner with a certified Korean engineering factory capable of delivering exceptional quality, custom alloy selection, and reliable global volume delivery. Talk to our technical engineering team today.
Get a Quote